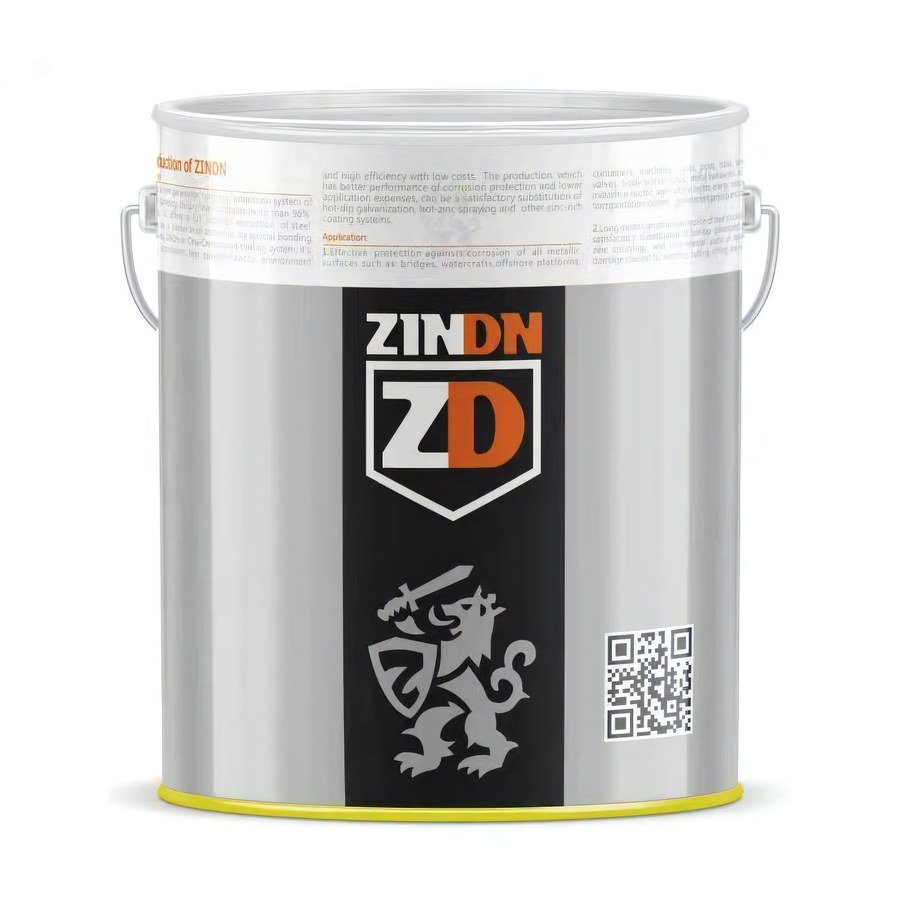
ZINDN Universal Epoxy Primer is an epoxy paint, used as a primer. Used for anti-corrosion of various parts of ship steel plate surfaces, suitable for ship ballast tanks, decks, outer plates, superstructures etc. A two-component ultra-high-solids epoxy paint cured by pure epoxy and polyamine adduct. Parameters on this page: volume solids 80 ± 3%, dry film thickness 100–250 µm / approx. 123–313 µm, theoretical spreading rate 5.63 m²/kg. Comparable products of the same brand: ZD6310-N01P Epoxy Oil-resistant Antistatic Primer, ZD6317 Fast-drying Zinc Phosphate Epoxy Paint, Hot-dip Galvanizing Special Epoxy Primer ZD6180.
Data source: ZINDN original Technical Data Sheet (TDS), "ZINDN Universal Epoxy Primer"; spreading rate and other values are converted from the TDS parameters, for selection reference only.
The above content is compiled from the manufacturer's datasheet and this site's parameter tables. For selection, coating systems and lead times, pleaseContact Usfor confirmation.
This page carries the full TDS for this product, translated from the manufacturer's original document. No file download is needed; for an original-language copy, send an enquiry.
| Volume Solids | 80 ± 3% |
|---|---|
| Dry Film Thickness | 100–250 µm / approx. 123–313 µm |
| Theoretical Spreading Rate | 5.63 m²/kg |
| VOC | 170 g/L |
| Density / Specific Gravity | Approx. 1.42 kg/L |
| Number of Components | Two-component |
| Thinner | Cleaner: ZINDN X-500 thinner |
| Mixing Ratio | Component B = 25.1:3.9 (by weight) |
| Packaging Specifications | Volume pack |
ZINDN High-solids Universal Epoxy 650
| Product overview | A two-component ultra-high-solids epoxy paint cured by pure epoxy and polyamine adduct |
|---|
Used for anti-corrosion of various parts of ship steel plate surfaces, suitable for ship ballast tanks, decks, outer plates, superstructures etc.
Used for anti-corrosion in atmospheric and immersed areas, suitable for petroleum refineries, power plants, steel structures and concrete bridges, and various equipment and facilities.
Compatible with most aged alkyd, chlorinated rubber and epoxy; can be used on water-blasted substrates; good compatibility with qualified shop primers.
| Product data | Colour | Grey, iron red (limited colour adjustment due to aluminium powder content) |
| (@20°C) | Gloss | Flat |
| Component B (curing agent) | High-solids Universal Epoxy 650GF Hardener | |
| Volume Solids | 80±3% | |
| Recommended dry film thickness | 100–250 µm / approx. 123–313 µm wet film thickness | |
| Theoretical Spreading Rate | 5.63 m²/kg, 8.0 m²/L (based on 100 µm dry film). | |
| Volatile Organic Compounds (VOC) | 170 g/L | |
| Density note | Approx. 1.42 kg/L |
Note: density figures are typical and vary with colour
| Drying data | Substrate Temperature | 5°C | 10°C | 23°C | 35°C |
| Touch dry | 10 h | 6 h | 3 h | 2 h | |
| Hard dry | 22 h | 15 h | 6 h | 4 h | |
| Fully cured | 21 days | 14 days | 5 days | 4 days | |
| Pot life | 5 h | 3.5 h | 2 h | 1.5 h | |
| Overcoating data | Substrate Temperature | 5°C | 10°C | 23°C | 35°C |
| Minimum recoat interval | 20 h | 12 h | 5 h | 3 h | |
| Maximum recoat interval | 28 days | 21 days | |||
Note: 1. The above data is for reference only; actual drying time and overcoating interval depend on film thickness, ventilation, humidity, underlying paint and mechanical strength etc. 2. Before overcoating, the film surface must be clean and dry, free of chalking and other contaminants; if necessary, the surface should be fully roughened before overcoating.
| Application parameters | Mixing: use a power mixer to stir Component A uniformly, then add Component B while stirring until fully mixed uniformly. |
|---|---|
| Induction time | At temperatures below 10 °C, induce for 15 minutes |
| Mixing ratio Component A | Component B = 25.1:3.9 (by weight) |
Thinner/cleaner: ZINDN X-500 thinner
| Nozzle pressure | 15~20MPa |
|---|---|
| Thinning ratio | 0–5% (by weight) |
Air spray: use suitable special equipment; thinning is required for spraying
Brush/roller: applicable, recommended for pre-coating and small-area application
| Application conditions | The substrate temperature shall be at least 3 °C above the air dew point, and the relative humidity below 85%. Temperature and humidity shall be measured on the substrate close to the work area. When applying in enclosed spaces, good ventilation is required to ensure normal drying of the film. |
|---|---|
| Surface Preparation | All surfaces to be coated shall be clean, dry and free of any contaminants. |
| Newbuilding | Remove weld spatter from the surface to be coated and grind welds and sharp edges smooth; welds and damaged areas of shop primer shall be blast cleaned to Sa 2.5 or power tool cleaned to St 3. Intact approved shop primer must be clean, dry and free of soluble salts and surface contaminants. Unapproved shop primer shall be blast cleaned to Sa 2.5 or consult ZINDN. |
| Overhaul | Blast clean the surface to Sa 2.5. |
| Repair/in-service maintenance | Blast clean damaged areas to Sa 2.5 or power tool clean to St 3. For blasted areas, apply the primer before oxidation occurs; if oxidation has occurred, the entire oxidized area must be re-blasted. |
| Coated steel plate surface | High-pressure water jet clean to WJ2L per SSPC VIS standard. |
| Typical coating systems | Hull outer plate: ZINDN High-solids Universal Epoxy 650 GF | 2×125 µm (dry film thickness) |
| Epoxy tie coat | 1×60 µm (dry film thickness) | |
| Tin-free self-polishing antifouling 860 GF | 2×100 µm (dry film thickness) | |
| Ballast tank: High-solids Universal Epoxy 650 GF | 2×160 µm (dry film thickness) |
For more application ranges, consult ZINDN.
| Safety and health | Before use, note the safety label on the packaging container, and refer to and follow the health and safety information, regulations and precautions in the ZINDN product Safety Data Sheet. During application and drying of this product, suitable ventilation and precautions must be taken to keep the solvent concentration within safe limits and prevent poisoning or oxygen deficiency. Take protective measures to avoid skin and eye contact with this product; in case of contact, wash immediately with a suitable cleaner, soap and water; if splashed into the eyes, rinse thoroughly with clean water and seek medical attention immediately. |
|---|
| Packaging Specifications | Pack size | Weight packaging | Volume pack |
| Component A 20 L | 25.1 kg | 16 L | |
| Component B 5 L | 3.9 kg | 4 L |
months; Component B shelf life is 24 months, then use after passing inspection.
| Precautions | Like all epoxy-based paints, this product will chalk and yellow when exposed to ultraviolet light. |
|---|---|
| Supplementary notes | Theoretical Spreading Rate |
| Dry film | Wet film | Theoretical Spreading Rate | |
| 100 µm | 125 µm | 5.63 m²/kg | 8.0 m²/L |
| 125 µm | 157 µm | 4.51 m²/kg | 6.40 m²/L |
| 160 µm | 200 µm | 3.52 m²/kg | 5.00 m²/L |
| 200 µm | 250 µm | 2.82 m²/kg | 4.00 m²/L |
| 250 µm | 313 µm | 2.25 m²/kg | 3.20 m²/L |
| Company declaration | The above product data is accumulated based on our experiments and practical application experience and can be used as an application guide. For applications carried out without our knowledge, we only guarantee the quality of the paint itself and are not responsible for any product performance problems in other aspects. We reserve the right to modify this data sheet according to continuous product improvement. |
|---|
Information is subject to the manufacturer's latest version; the manufacturer's latest TDS prevails.
The technical parameters on this page are taken from the product's original manufacturer technical datasheet, the copyright of which belongs to the manufacturer. If a rights holder considers the presentation inappropriate, contact us for verification and handling.
For more Q&A on selection, application, acceptance and defect diagnosis, seeFAQsection.
Packaging specifications and batch lead times are subject to actual availability. PleaseContact Uscontact us for project-based calculation.