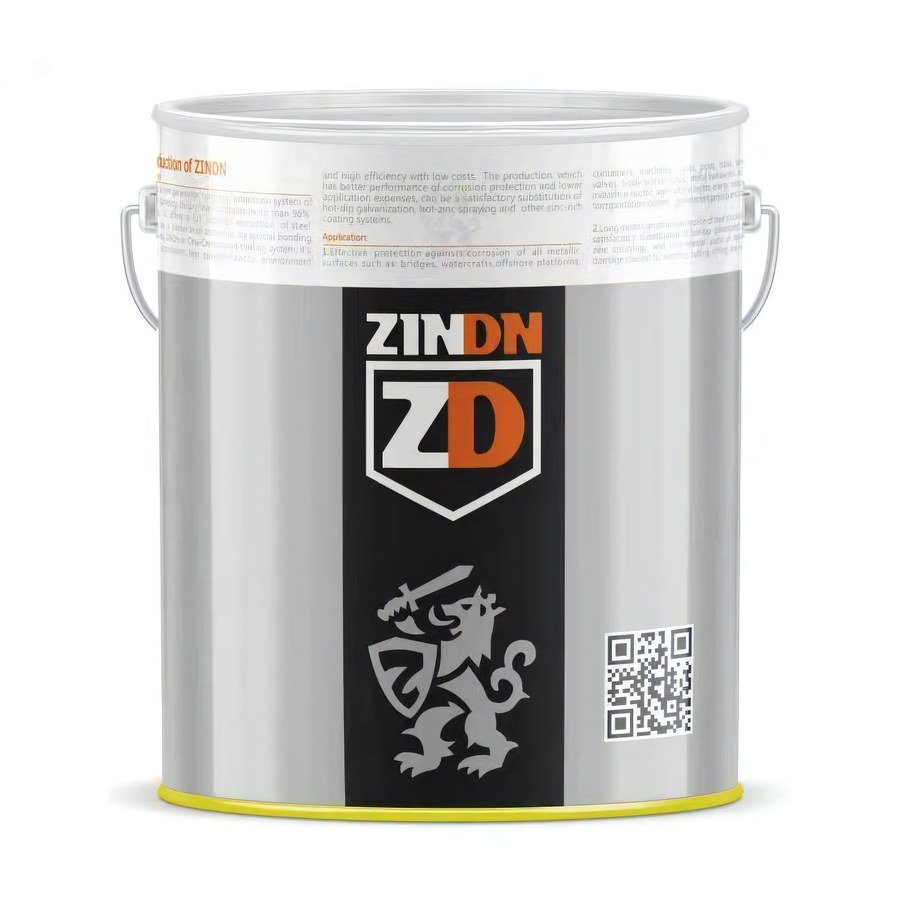
ZD6310-Z4600 Cold Spray Graphene Zinc Coating belongs to cold galvanizing. For maintenance, its cathodic protection anti-corrosion effect is achieved only when applied to surfaces prepared to bare steel. A two-component high-solids heavy-duty anti-corrosion coating composed of specially modified resin, pure thin graphene, zinc powder, inorganic fillers, solvents, additives, etc. Parameters on this page: volume solids 61 ± 2%, dry film thickness 40/80/120 µm, theoretical spreading rate 0.44 kg/m². Comparable products of the same brand: ZD6310-Z850 Cold Spray Graphene Zinc Coating, ZZ96-T Zhuozhu Cold Galvanizing, ZINDN Cold Galvanizing ZD96-1.
Parameter source: ZINDN original technical data sheet (TDS) "ZD6310-Z4600 Cold Spray Graphene Zinc Coating"; values such as spreading rate are converted from TDS parameters and are for selection reference only.
The above content is compiled from the manufacturer's datasheet and this site's parameter tables. For selection, coating systems and lead times, pleaseContact Usfor confirmation.
This page carries the full TDS for this product, translated from the manufacturer's original document. No file download is needed; for an original-language copy, send an enquiry.
| Volume Solids | 61 ± 2% |
|---|---|
| Dry Film Thickness | 40/80/120 µm |
| Theoretical Spreading Rate | 0.44 kg/m² |
| VOC | ≤340g/L |
| Density / Specific Gravity | 2.2 ± 0.1 |
| Number of Components | Two-component |
| Flash Point | >25 °C (mixture) |
| Thinner | X-500 Thinner |
| Mixing Ratio | Component A (base) : Component B (curing agent) = 32:3 |
ZD6310-Z4600 Cold Spray Graphene Zinc Coating
A two-component, high-solids heavy-duty anticorrosive coating composed of special modified resin, pure thin graphene, zinc dust, inorganic fillers, solvents and additives.
Complies with the performance standard HG/T 5573-2019 Graphene Zinc Dust Coatings;
Pure thin nano-graphene provides dual functions of lamellar barrier and activated zinc powder;
High spreading rate, saving roughly 15% paint consumption compared with epoxy zinc-rich;
Mature and stable coating systems, high adhesion and high application tolerance;
The film has excellent anti-rust performance and can replace traditional coating materials such as epoxy zinc-rich in C4, C5, CX and other environments;
As a primer for blast-cleaned bare steel in medium to severe corrosive environments, such as steel structures, bridges, port machinery, offshore platforms, construction machinery, storage tanks, pipelines and power facilities. Used with high-performance paints, it further improves the anti-corrosion performance of the coating system;
Suitable for approved zinc-rich shop primer surfaces to be retained;
Suitable for repair of damaged areas of galvanised parts or zinc silicate primer coatings;
For maintenance, its cathodic protection anti-corrosion effect is achieved only on surfaces prepared to bare steel.
| Colour | Dark grey |
|---|---|
| Gloss | Matt |
| Volume Solids | 61±2% |
| Mixed density (kg/L) | 2.2±0.1 |
| Dry film thickness (µm) | Minimum 40 | Typical 80 | Maximum 120 |
| Wet film thickness (µm) | 66 | 131 | 197 |
| Theoretical spreading rate (kg/m²) | 0.15 | 0.29 | 0.44 |
| Practical Spreading Rate | Allowing for a suitable loss factor |
|---|---|
| VOC content | ≤340g/L |
| New steel | Remove grease from the surface with a suitable cleaner, and rinse off salts and other contaminants with fresh water. Remove weld slag, and grind welds and sharp edges smooth. Abrasive blast clean to Sa 2.5 (ISO 8501-1); the ideal surface roughness is Rz 30–75 µm (medium roughness on the ISO 8503-1 comparator). Apply the primer within 4 hours of blast cleaning. |
|---|---|
| Shop-primed surface | Welds, heat-treated areas and damaged areas must be blast cleaned to Sa 2.5 (ISO 8501-1) or cleaned with power tools to St 3. Only sound, approved zinc-rich shop primer may be retained. When exposed to humid conditions, zinc salts form on the zinc-rich primer surface; before recoating, remove soluble zinc salts with fresh water and remove white rust (zinc corrosion products) with a stiff brush. If the zinc-rich primer is damaged over a large area, full blast cleaning is recommended. |
| Repair | Thoroughly remove grease from the surface with a suitable cleaner, and wash off salts and other contaminants with high-pressure fresh water. Remove rust and other loose material by blast cleaning; alternatively, grind small rusted areas with power tools and touch up bare areas with this product. |
Application environment temperature 5–38 °C, relative humidity not more than 85%, and the steel surface temperature should be at least 3 °C above the dew point. Do not apply outdoors in adverse weather such as rain, fog, snow, strong wind and heavy dust;
In hot summer weather, guard against dry spray; provide ample ventilation during application and drying in confined spaces;
| Mixing | This product is supplied as two containers forming one unit. Stir the base thoroughly with a power mixer, add the curing agent in the specified ratio, stir again with a power mixer, and add the recommended thinner to adjust to a suitable application viscosity. Once mixed, use within the specified pot life. |
|---|---|
| Thinner / Cleaning Solvent | X-500 Thinner |
| Mixing ratio (by weight) | Component A (base) : Component B (curing agent) = 32:3 |
| Induction Time | 20 min (25 °C) |
| 5°C | 15°C | 25°C | 35°C |
| 6 h | 5 h | 4 h | 3 h |
| Application Methods | Airless spray and air spray are recommended; brush and roller are recommended only for touch-up, small-area application or repair. |
|---|
Stir frequently during application to prevent settling of the zinc dust.
| Application Methods | Unit | High-pressure airless spray | Air Spray | Brush/roller |
| Spray gun tip size | mm | 0.43~0.53 | 1.8~2.2 | —— |
| Spray pressure | kg/cm² | 150~200 | 3~4 | —— |
| Thinning quantity | % | 0~10 | 10~20 | 5~10 |
| Substrate surface temperature | 5°C | 15°C | 25°C | 35°C |
| Surface Dry | 5 h | 2 h | 30 min | 10 min |
| Hard Dry | 24 h | 20 h | 14 h | 10 h |
| Minimum recoat interval | 20 h | 15 h | 10 h | 6 h |
| Maximum recoat interval | Before applying the next coat, the surface must be clean, dry and free of zinc salts and contaminants. Note: the above data are measured under well-ventilated conditions, at typical film thickness and 75% relative humidity, and are for reference only. |
|---|
Actual drying times and the interval before recoating may be longer or shorter depending on film thickness, ventilation, humidity, the underlying paint, requirements for early handling and mechanical strength, and other factors.
| Preceding coat | Apply directly to steel surfaces prepared to Sa2.5 or St3, or to approved shop primer surfaces. |
|---|---|
| Subsequent coat | Epoxy and chlorinated rubber coatings must not be used with alkyd coatings |
| Packaging Specifications | Component A 32 kg, Component B 3 kg |
|---|---|
| Flash Point | >25 °C (mixture) |
| Storage conditions | Store in accordance with national regulations. Keep at a temperature above 0 °C in a dry, cool, well-ventilated place away from heat and sources of ignition. Keep containers tightly closed. |
This product contains flammable materials; site safety must comply with the relevant national or local regulations. Read the safety labels on the packaging and the product Safety Data Sheet (MSDS).
Avoid inhaling solvent vapours and spray mist, avoid contact of paint with skin and eyes, and do not swallow the product. Take the necessary precautions and protective measures for fire prevention, explosion prevention and environmental protection. Use only in well-ventilated conditions. In confined or poorly ventilated areas, provide forced ventilation.
Waste disposal must comply with the relevant national or local regulations.
The information and data in this document are accumulated from our tests and practical experience and may serve as an application guide. Since the use of the product is generally beyond our control, we guarantee only the quality of the product itself. We reserve the right to modify this document without prior notice as the product is improved.
| Version information | Published in September 2023; this data sheet supersedes all previous versions |
|---|
Information is subject to the manufacturer's latest version; the manufacturer's latest TDS prevails.
The technical parameters on this page are taken from the product's original manufacturer technical datasheet, the copyright of which belongs to the manufacturer. If a rights holder considers the presentation inappropriate, contact us for verification and handling.
For more Q&A on selection, application, acceptance and defect diagnosis, seeFAQsection.
Packaging specifications and batch lead times are subject to actual availability. PleaseContact Uscontact us for project-based calculation.