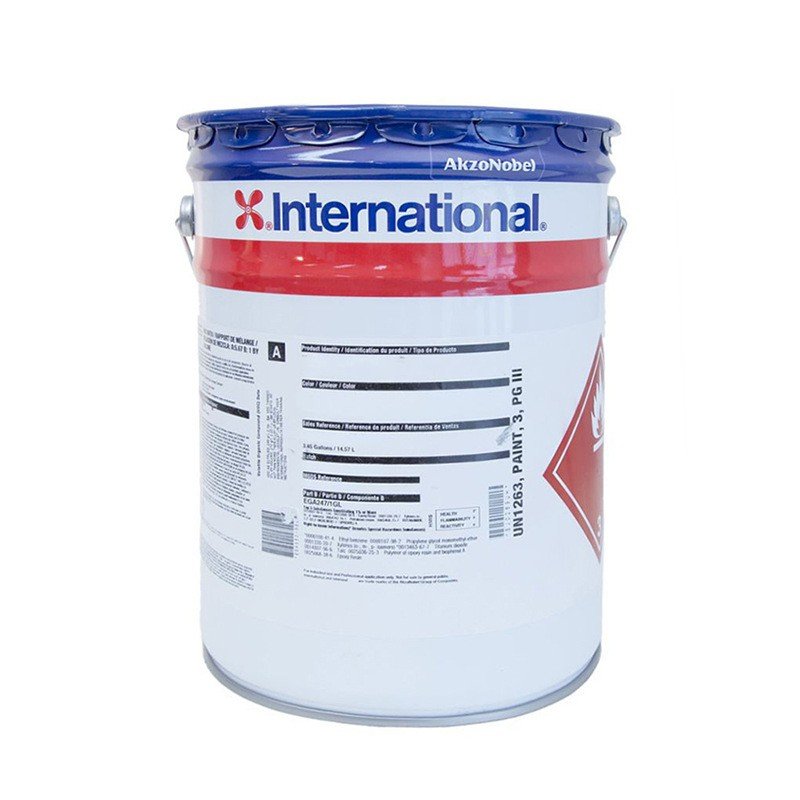
Interline 921 Universal Filler Compound is an epoxy coating. Interline 921 has a very long recoat interval, adding flexibility in operation and allowing applicators to schedule work better and return tanks to service quickly. A two-component, solvent-free, chemically resistant epoxy phenolic filler compound, formulated for easy application and offering great flexibility in tank lining work. Because of pot life limitations, airless spray with plural-component equipment normally requires application at temperatures above 25 °C (77 °F). Parameters on this page: volume solids 100%; dry film thickness 1000–4000 µm (40–160 mils); theoretical spreading rate 0.50 m²/L.
Source: AKZONOBEL original technical data sheet (TDS) 'Interline 921 Universal Filler Compound'. Spreading rate and other values converted from the TDS; for reference only.
The above content is compiled from the manufacturer's datasheet and this site's parameter tables. For selection, coating systems and lead times, pleaseContact Usfor confirmation.
This page carries the full TDS for this product, translated from the manufacturer's original document. No file download is needed; for an original-language copy, send an enquiry.
| Volume Solids | 100% |
|---|---|
| Dry Film Thickness | 1000–4000 µm (40–160 mils) |
| Theoretical Spreading Rate | 0.50 m²/L |
| VOC | 0.75 lb/gal (90 g/L), US EPA Method 24, 38 … |
| Density / Specific Gravity | 1.30 kg/L (10.8 lb/gal) |
| Number of Components | Two-component |
| Thinner | Not applicable. Do not thin |
| Mixing Ratio | 2 parts : 1 part (by volume) |
| Colour / Appearance | Cream, INTERLINE 921 |
For more Q&A on selection, application, acceptance and defect diagnosis, seeFAQsection.
A two-component, solvent-free, chemically resistant epoxy phenolic filler compound, formulated for easy application and offering great flexibility in tank lining work.
As a universal filler compound, it is suitable for application with ordinary airless spray equipment, for new tanks or refurbishment of corroded tanks. Interline 921 has a very long recoat interval, adding flexibility in operation and allowing applicators to schedule work better and return tanks to service quickly.
Interline 921 filler compound is used to treat welds, overlaps, coamings and other surface irregularities, providing a smooth, even transition between uneven surfaces before applying the Interline glass fibre reinforced laminate system.
| Colour | Cream, INTERLINE 921 |
|---|---|
| Gloss | N/A |
| Volume Solids | 100% |
| Typical thickness | Dry film thickness 1000–4000 µm (40–160 mils), equivalent to wet film thickness 1000–4000 µm (40–160 mils) |
| Theoretical Spreading Rate | At 2000 µm dry film thickness and the stated volume solids: 0.50 m²/L; at 80 mils dry film thickness and the stated volume solids: 20 ft²/US gal. Note: the actual applied thickness depends on the surface condition and shape of the steel to be coated |
| Practical Spreading Rate | Allowing for a suitable loss factor |
| Application Methods | Airless spray, plural-component airless spray; for drying time refer to the recommended topcoat recoat interval |
| Temperature | Surface Dry | Hard Dry | Minimum | Maximum |
| 10°C (50°F) | 10 h | 36 h | 28 days | |
| 15°C (59°F) | 9 h | 20 h | 28 days | |
| 25°C (77°F) | 6 h | 12 h | 28 days | |
| 40°C (104°F) | 2 h | 5 h | 10 days | |
| Flash point (typical) | Component A >101 °C (214 °F); Component B 49 °C (120 °F); mixed 75 °C (167 °F) |
|---|---|
| Product weight | 1.30 kg/L (10.8 lb/gal) |
| Volatile Organic Compounds | 0.75 lb/gal (90 g/L), US EPA Method 24; 38 g/kg, EU Solvent Emissions Directive (Council Directive 2010/75/EU). For more details, refer to the 'Product Characteristics' section. |
All surfaces to be coated must be clean, dry and free of contaminants. Before application, all surfaces must be assessed and prepared in accordance with ISO 8504:2000.
Oil and grease must be removed in accordance with the SSPC-SP1 solvent cleaning standard.
Abrasive blasting: the product shall be applied only to surfaces abrasive-blast-cleaned to Sa2½ (ISO 8501-1:2007) or SSPC SP10. A sharp, angular surface profile of 75–100 µm (3–4 mil) is recommended.
Interline 921 must be applied before the steel oxidizes. If oxidation has occurred, the entire oxidized area should be re-blasted to the standard above. Surface defects exposed during blasting should be ground, filled or treated by an appropriate method.
Where permitted by local VOC regulations, Interline 982 may be applied as a primer before oxidation occurs, at a dry film thickness of 15–25 µm (0.6–1.0 mil). Dehumidification may also be used to maintain the blast standard.
Interline 982 keeps the blast standard on tank interiors in a semi-protected environment for up to 28 days. If moisture is present on the surface, oxidation occurs and re-blasting is required.
| Mixing | For tank application, Interline 921 must be applied in accordance with the International Protective Coatings application guide. The coating is supplied as a set in two cans. Always mix the complete set in the supplied ratio. Once mixed, use the set within the specified pot life. |
|---|
(1) Stir the base (Component A) with a power mixer.
(2) Stir the curing agent (Component B) with a power mixer.
(3) Mix all of the curing agent (Component B) with the base (Component A) and stir thoroughly with a mixer.
| Mixing ratio | 2 parts : 1 part (by volume) |
|---|
| Pot life | 10°C (50°F) | 15°C (59°F) | 25°C (77°F) | 40°C (104°F) |
| 60 min | 50 min | 30 min | 15 min |
| Plural-component airless spray | Suitable: consult International Industrial Coatings for specific recommendations. See Product Characteristics. |
|---|---|
| Suitable for airless spray | Recommended nozzle tip 0.66–0.79 mm (26–31 thousandths of an inch); total paint pressure at the nozzle not less than 211 kg/cm² (3000 lb/in²) |
| Air Spray | Not recommended (with pressure pot) |
| Brush | N/A |
| Roller application | N/A |
| Thinner | Not applicable. Do not thin |
| Cleaner | International GTA853 or International GTA415 |
| Interruption of work | Paint must not be left in hoses, spray guns or spray equipment. Flush all equipment thoroughly with International thinner. Once mixed, paint should not be resealed; if work is interrupted for too long, mix a fresh batch before resuming application. |
| Cleaning | All equipment should be cleaned immediately after use with International thinner. Flushing spray equipment periodically during the daily work is good working practice. Cleaning frequency depends on the volume sprayed, temperature and time spent, including delays. |
All surplus paint and empty containers must be disposed of in accordance with the appropriate local regulations/laws.
Apply by airless spray only. Other methods such as brush or roller may require more than one coat and are recommended only for small areas or initial stripe coating.
When the temperature of Interline 921 is kept between 15–25 °C (59–77 °F), ordinary 63:1 airless spray equipment can be used. At lower temperatures, a suitably pressurized line heater can be used to assist extraction and atomization. In addition, Interline 921 is suitable for application with plural-component airless spray equipment capable of accurate ratio metering, allowing more flexible application at high temperature.
Because of pot life limitations, airless spray with plural-component equipment normally requires application at temperatures above 25 °C (77 °F).
Heavily pitted areas should be pre-coated by brush to ensure good surface wetting.
Apply by hand trowel or extrusion to fill deep pitted areas, providing a uniform surface flush with the adjoining surfaces.
The temperature of the surface to be coated must be at least 3 °C (5 °F) above the dew point.
Do not apply when the steel temperature is below 10 °C (50 °F).
The climatic conditions inside the tank must be controlled, keeping the maximum relative humidity at 70% at any temperature.
Unacceptably low temperature and/or high humidity during or immediately after application leads to incomplete curing and surface contamination, compromising intercoat adhesion.
Note: VOC values are typical and for guidance only. They may vary with colour and general production tolerances.
Interline 921 can be applied directly to correctly prepared bare steel. It is also suitable for application over the following primers: Interline 982. Interline 921 is normally overcoated with itself or with Interline 984 as the topcoat. For other primers/topcoats, consult International Industrial Coatings.
Consult International Industrial Coatings to confirm that Interline 921 is suitable for contact with the product to be stored.
| For further information on the industry standards, terms and abbreviations used in this datasheet, see www.international-pc.com | In the following documents on the website: • Definitions and abbreviations • Surface preparation • Coating application • Theoretical and practical spreading rate |
|---|---|
| • Interline 984 | 'Technical package for the glass fibre reinforced coating system'. The contents of these sections are also available as separate booklets on request. |
This product is intended for professional applicators in industrial use only.
All work, including the application and use of this product, must comply with the relevant national standards, laws and regulations on safety, health and environmental protection.
During application and the subsequent drying period (for common drying times, see the product data sheet), provide adequate ventilation to keep solvent concentrations within safe limits and prevent fire and explosion. Forced ventilation is required in confined spaces. During application and drying, personal ventilation and respiratory protection (e.g. air-fed hood or suitable filter mask) must also be provided. Take the necessary measures to prevent skin and eye contact with the coating (e.g. protective clothing, gloves, goggles, mask, barrier cream).
Before use, read and follow the Material Safety Data Sheet and the Health and Safety section of the application procedure for this product (for two-component coatings, those of the base and curing agent).
If welding or cutting is performed on metal substrate previously coated with this product, dust and fumes will be released; use suitable personal protective equipment and local exhaust ventilation.
The specific safety measures depend on the application method and working environment. If these warnings or instructions are not fully understood or cannot be strictly observed, do not use the product and consult International Paint.
Warning: this product contains liquid epoxy and modified polyamines and may cause skin sensitisation if handled improperly.
| Packaging Specifications | Component A | Component B | ||
| Volume | Packaging | Volume | Packaging | |
| 18 L | 12 L | 20 L | 6 L | 10 L |
| 3 US gal | 2 US gal | 5 US gal | 1 US gal | |
For other packaging sizes, contact AkzoNobel.
| Packaging Specifications | Component A | Component B |
| 18 L | 16.64 kg | 10.02 kg |
| 3 US gal | 24.2 lb | 12.8 lb |
| U.N. shipping number | UN3082 (base) : UN2924 (curing agent) |
|---|
| Shelf life | At 25 °C (77 °F), a minimum of 18 months, after which inspection is required. Store in a dry, cool place away from heat sources and ignition sources. International Paint recommends always storing the product above 10 °C (50 °F) to ensure its stability. |
|---|
© 2024/2/26 AkzoNobel. All rights reserved.
All registered trademarks mentioned in this publication are licensed to or owned by AkzoNobel.
www.international-pc.com
Information is subject to the manufacturer's latest version; the manufacturer's latest TDS prevails.
The technical parameters on this page are taken from the product's original manufacturer technical datasheet, the copyright of which belongs to the manufacturer. If a rights holder considers the presentation inappropriate, contact us for verification and handling.
Packaging specifications and batch lead times are subject to actual availability. PleaseContact Uscontact us for project-based calculation.