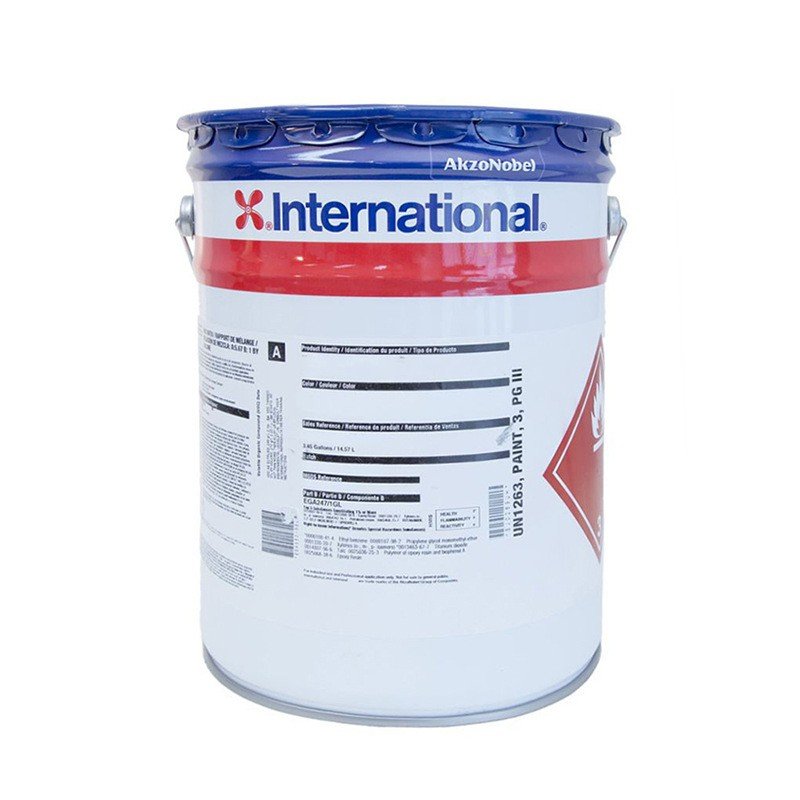
Intergard 269 Epoxy Primer / Tie Coat is an epoxy coating used as a primer. It can also be used as a tie coat over zinc silicate coatings to prevent zinc salt formation on aged coatings and pinholes in subsequent high-build topcoats. Recoatable even after extended ageing. When coating steel at high ambient temperature, thinning with International thinner may be required to prevent dry spray and control film thickness. This product cannot fully cure below 5 °C (41 °F). Parameters on this page: theoretical spreading rate 11.80 m²/L; number of components: two.
Source: AKZONOBEL original technical data sheet (TDS) 'Intergard 269 Epoxy Primer / Tie Coat'. Spreading rate and other values converted from the TDS; for reference only.
The above content is compiled from the manufacturer's datasheet and this site's parameter tables. For selection, coating systems and lead times, pleaseContact Usfor confirmation.
This page carries the full TDS for this product, translated from the manufacturer's original document. No file download is needed; for an original-language copy, send an enquiry.
| Volume Solids | 47% |
|---|---|
| Dry Film Thickness | — |
| Theoretical Spreading Rate | 11.80 m²/L |
| VOC | 3.75 lb/gal (450 g/L), US EPA Method 24, 293… |
| Density / Specific Gravity | 1.53 kg/L (12.8 lb/gal) |
| Number of Components | Two-component |
| Thinner | Do not exceed the thinning limits of local environmental regulations |
| Mixing Ratio | 4 parts : 1 part (by volume) |
| Colour / Appearance | Red (for more details, refer to the 'Product Characteristics' section) INTERGAR… |
For more Q&A on selection, application, acceptance and defect diagnosis, seeFAQsection.
A two-component, fast-drying epoxy primer.
Can be recoated after long-term ageing.
As a holding primer over blast-cleaned steel, suitable for immersion and exposed service, and compatible with other products in various high-performance anti-corrosion systems.
Suitable for both new structures and maintenance of existing metal structures.
May also be used as a tie coat over zinc silicate coatings, preventing zinc salt formation on aged coatings and pinholes in subsequent high-build topcoats.
| Colour | Red (for more details, refer to the 'Product Characteristics' section) INTERGARD 269 |
|---|---|
| Gloss | Matt |
| Volume Solids | 47% |
| Typical thickness | 40 µm (1.6 mil) DFT corresponds to 85 µm (3.4 mil) WFT |
| Theoretical Spreading Rate | 11.80 m²/L at 40 µm dry film thickness and the stated volume solids; 471 ft²/US gal at 1.6 mil dry film thickness and the stated volume solids |
| Practical Spreading Rate | Allowing for a suitable loss factor |
| Application Methods | Suitable for airless spray, air spray, brush, roller. Drying time; recommended topcoat recoat interval |
| Temperature | Surface Dry | Hard Dry | Minimum | Maximum |
| 10°C (50°F) | 40 min | 16 h | 16 h² | Unlimited¹ |
| 15°C (59°F) | 35 min | 12 h | 12 h² | Unlimited¹ |
| 25°C (77°F) | 30 min | 8 h | 8 h² | Unlimited¹ |
| 40°C (104°F) | 15 min | 1 h | 4 h² | Unlimited¹ |
¹ When polysiloxane topcoats are used, the maximum recoat interval is reduced. For details, consult International Paint.
² When Intergard 269 is used as a primer for tank lining products, the recoat interval depends on the lining product to be overcoated. Refer to the relevant product data sheet for more information.
| Flash point (typical) | Component A 26 °C (79 °F); Component B 25 °C (77 °F); mixed 26 °C (79 °F) |
|---|---|
| Product weight | 1.53 kg/L (12.8 lb/gal) |
| Volatile Organic Compounds | 3.75 lb/gal (450 g/L), US EPA Method 24; 293 g/kg, EU Solvent Emissions Directive (Council Directive 2010/75/EU); coating hazard GB 30981.2-S-Pb≤1000-NC; complies with GB 30981.2-2025. For more details, refer to the 'Product Characteristics' section. |
All surfaces to be coated must be clean, dry and free of contaminants. Before application, all surfaces must be assessed and prepared in accordance with ISO 8504:2019.
Oil and grease must be removed in accordance with the SSPC-SP1 solvent cleaning standard.
Blasting: for immersion service, apply Intergard 269 over surfaces blast-cleaned to Sa 2½ (ISO 8501-1:2007) or SSPC SP10. However, for atmospheric exposure, apply Intergard 269 over surfaces blasted to Sa 2½ (ISO 8501-1:2007) or at least SSPC SP6.
Surface defects exposed by blast cleaning must be ground, filled or treated by a suitable method.
Ultra-high-pressure water jetting (for non-immersion use only) may be applied over surfaces prepared to Sa2 (ISO 8501-1:2007) or SSPC SP6, with light rust allowed to a standard not lower than HB2M (see the International Paint hydroblasting standard). For more information, contact International Paint.
Application as a tie coat (see Product Characteristics): with a zinc-rich primer, remove weld spatter where necessary, smooth welds and sharp edges, and blast-clean welds and damaged primer to Sa 2½ (ISO 8501-1:2007) or SSPC SP6. Shop-primed or other primer surfaces must be dry and free of contaminants (oil, grease, salts) and recoated with Intergard 269 within the specified primer recoat interval (refer to the relevant data sheet).
Before overcoating, ensure the zinc dust primer is fully cured, and clean, dry and free from zinc salts.
| Mixing | This product is supplied in two containers forming one unit. Mix the two components in the specified ratio in one operation. Once mixed, use within the specified pot life. |
|---|
(1) Stir the base (Component A) with a power mixer.
(2) Mix all of the curing agent (Component B) with the base (Component A) and stir thoroughly with a power mixer.
| Mixing ratio | 4 parts : 1 part (by volume) |
|---|
| Pot life | 10°C (50°F) | 15°C (59°F) | 25°C (77°F) | 40°C (104°F) |
| 17 h | 12 h | 8 h | 3 h |
| Suitable for airless spray | Recommended nozzle tip size 0.38–0.53 mm (15–21 thou); total paint pressure at the nozzle not less than 141 kg/cm² (2005 psi) |
|---|
| Air Spray | Recommended | Spray gun | DeVilbiss MBC or JGA |
| Air nozzle | 704 or 765 | ||
| (with pressure pot) | Nozzle | E | |
| Brush | Applicable — for small-area repair only | Typical thickness 25–30 µm (1.0–1.2 mils) | |
| Roller application | Applicable — for small-area repair only | Typical thickness 25–30 µm (1.0–1.2 mils) | |
| Thinner | International GTA220 | Do not exceed the thinning limits of local environmental regulations |
(or International GTA415)
| Cleaner | Use a cleaning solvent that complies with local regulations. Consult the local representative for specific recommendations. |
|---|---|
| Interruption of work | Do not leave paint in hoses, spray guns or spray equipment. Flush all equipment thoroughly with International thinner. |
Mixed paint should not be resealed. If work is interrupted for too long, mix a fresh batch of paint for application.
| Cleaning | All equipment should be cleaned immediately after use with International thinner. Flushing spray equipment periodically during daily work is good practice. Cleaning frequency depends on the volume sprayed, temperature, spraying time, including interruptions, and other factors. |
|---|
Surplus paint and empty containers must be disposed of in accordance with the relevant regional regulations.
Use as a temporary protective primer: Intergard 269 is suitable as a blast temporary protective primer for steel structures in immersion and atmospheric environments. Apply Intergard 269 to the recommended thickness, as over-application produces a glossy surface unsuitable for recoating after ageing.
When coating steel at high ambient temperatures, thinning with International thinner may be required to prevent dry spray and control film thickness. This product does not cure adequately below 5 °C (41 °F). For optimum performance, curing should take place above 10 °C (50 °F).
Intergard 269 is also suitable for application over degreased and abraded stainless steel and galvanized steel. Abrade by light blasting with non-metallic abrasive; for small areas, use an emery wheel. As a tie coat: to ensure good penetration of the zinc silicate, thin Intergard 269 15–25% with International thinner. Intergard 269 must cure before the high-build topcoat is applied, otherwise its pinhole prevention is less effective.
Avoid excessive film thickness, otherwise cracking may occur when recoated with a high-build coating.
For application below 10 °C (50 °F), other tie coats are available. Contact International Paint for information.
For marine environments, the system and recoat intervals may differ.
Use as a temporary protective primer for tank lining products: Intergard 269 can be used as a temporary protective primer for selected tank lining products, only for storage of crude oil/water mixtures and refined hydrocarbon cargoes.
Refer to the relevant product data sheet for surface preparation and recoating recommendations. Contact the local AkzoNobel representative to confirm specifications and service limitations.
Red Intergard 269 is available worldwide; other colours can be supplied on request. For details, consult International Industrial Coatings.
Note: the VOC value given is based on the maximum possible value for the product and may vary with colour and general production tolerances.
Although the low-molecular-weight reactive additive becomes part of the film when cured under normal ambient conditions, analysis by EPA Method 24 shows that it also affects the VOC value.
Intergard 269 is suitable for application over the following primers: Interzinc 22, Interzinc 52. The following topcoats/intermediate coats are recommended for use with Intergard 269:
| Intercure 200HS | Intergard 740 |
|---|---|
| Intercure 420 | Interseal 670HS |
| Interfine 629HS | Interthane 870 |
| Interfine 878 | Interthane 990 |
| Interfine 979 | Interthane 990E |
| Intergard 251 | Interzone 505 |
| Intergard 345 | Interzone 954 |
| Intergard 475HS | Interzone 1000. Intergard 269 can be used as a temporary protective primer for selected tank lining products: Interline 984, Interline 925P, Interline 955 |
| For further information on the industry standards, terms and abbreviations used in this datasheet, see www.international-pc.com | In the following documents on the website: • Definitions and abbreviations • Surface preparation • Coating application • Theoretical and practical spreading rate. These sections are also available as separate publications on request. |
|---|
This product must be applied at the production site by professional applicators in accordance with the recommendations in this manual, the Material Safety Data Sheet and the instructions on the container label. Do not use this product without first reviewing the Material Safety Data Sheet (MSDS) that International Paint provides for its customers.
All work related to the application and use of this product must be carried out in accordance with the relevant national health, safety and environmental standards and regulations.
If welding or flame cutting is required on metal coated with this product, dust and fumes will be generated; use appropriate personal protective equipment and adequate local ventilation.
If in doubt about the suitability of this product for the intended use, consult AkzoNobel for further advice.
| Packaging Specifications | Component A | Component B | ||
| Volume | Packaging | Volume | Packaging | |
| 20 L | 16 L | 20 L | 4 L | 5 L |
| 5 US gal | 4 US gal | 5 US gal | 1 US gal | |
For other packaging sizes, contact AkzoNobel.
| Packaging Specifications | Component A | Component B |
| 20 L | 28.9 kg | 4.1 kg |
| 5 US gal | 59.7 lb | 8.4 lb |
| Shelf life | At 25 °C (77 °F): component A 12 months, component B 18 months; inspect thereafter. Store in a dry, cool environment away from heat and ignition sources. |
|---|
© 2026/5/26 AkzoNobel. All rights reserved.
All registered trademarks mentioned in this publication are licensed to or owned by AkzoNobel.
www.international-pc.com
Information is subject to the manufacturer's latest version; the manufacturer's latest TDS prevails.
The technical parameters on this page are taken from the product's original manufacturer technical datasheet, the copyright of which belongs to the manufacturer. If a rights holder considers the presentation inappropriate, contact us for verification and handling.
Packaging specifications and batch lead times are subject to actual availability. PleaseContact Uscontact us for project-based calculation.
The factory item numbers of Intergard 269 Epoxy Primer / Tie Coat are as follows.Item No.is the most accurate form when ordering;Colour/colour codecorresponds to the actual colour (RAL, GSB are colour chart codes);Packaging SpecificationsFactory complete-set specification format. Colors not listed may be ordered against the colour card.
| Item No. | Colour / colour code | Packaging Specifications |
|---|---|---|
| EGA088 | Red | 16 L + 4 L |
| EGA077 | Off White | 20 L |
This model has a total of2item numbers, all listed on this page; colours outside the table (including special colours and bulk packaging) can be confirmed by phone, delivery dates are advised according to the factory's current production schedule and stock. In the packaging specification, the "+" indicates the complete-set notation for two-component products (base + curing agent), subject to the factory specification; a "—" in the colour column denotes an auxiliary product, or that the item has no colour code in the factory system.