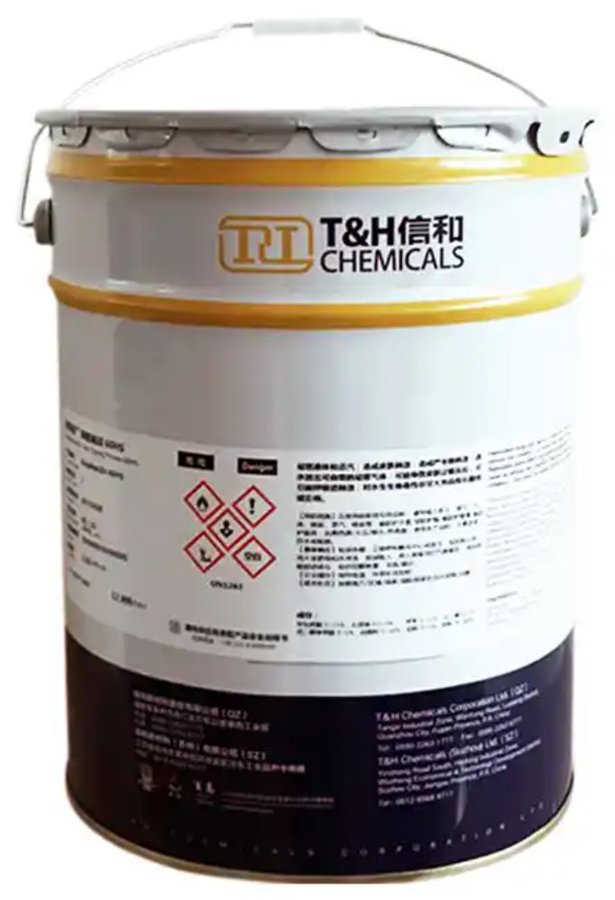
High-solids Epoxy MIO Intermediate Coat XH4067 is an epoxy coating used as an intermediate coat. In severely corrosive atmospheric environments, it can be used as an intermediate coat on new construction or maintenance work to improve the barrier protection of various anticorrosive systems. Parameters on this page: volume solids 81 ± 2%; dry film thickness 80/120/160 µm; theoretical spreading rate 5 m²/L.
Parameter source: T&H original technical data sheet (TDS) for High-solids Epoxy Micaceous Iron Oxide Intermediate Coat XH4067; spreading rate and other values are converted from TDS parameters and provided for product selection reference only.
The above content is compiled from the manufacturer's datasheet and this site's parameter tables. For selection, coating systems and lead times, pleaseContact Usfor confirmation.
This page carries the full TDS for this product, translated from the manufacturer's original document. No file download is needed; for an original-language copy, send an enquiry.
| Volume Solids | 81 ± 2% |
|---|---|
| Dry Film Thickness | 80/120/160 µm |
| Theoretical Spreading Rate | 5 m2/L |
| VOC | 240g/L |
| Density / Specific Gravity | 1.81 kg/L |
| Number of Components | Two-component |
| Flash Point | 25°C |
| Thinner | 0-15% |
| Mixing Ratio | Base : curing agent = 77:23 (by volume) |
For more Q&A on selection, application, acceptance and defect diagnosis, seeFAQsection.
A high-solids, high-build epoxy intermediate coat containing micaceous iron oxide pigment. In severely corrosive atmospheric environments, it can be used as an intermediate coat on new construction or maintenance work to improve the barrier protection of various anticorrosive systems.
| Colour | MIO grey |
|---|---|
| Gloss | Flat |
| density | 1.81 kg/L |
| Volume Solids | 81±2% |
| Volatile Organic Compounds | 240g/L |
| Flash Point | 25°C |
| Mixing ratio | Base : curing agent = 77:23 (by volume) |
| Typical dry film thickness | 100µm |
|---|---|
| Recommended dry film thickness | 75–200 µm, depending on system requirements |
| Thinner quantity (by volume) | Airless spray 0–5% | Air spray 5–10% | Roller or brush 0–15% |
| Recommended nozzle size | 0.43~0.65mm | 1.5~2.5mm | None |
| Recommended spray pressure | 20~25MPa | 0.3~0.6MPa | None |
| Application suitability | Recommended | Applicable | Suitable for small-area repair |
*In hot seasons, the slow-drying thinner XH9400S is recommended
| Dry film thickness (µm) | 80 | 120 | 160 |
| Wet film thickness (µm) | 100 | 150 | 200 |
| Theoretical spreading rate (m²/L) | 10 | 6.6 | 5 |
| Temperature | Surface Dry | Hard Dry | Pot Life | Recoat interval | |
| Minimum | Maximum* | ||||
| 5°C | 12h | 30h | 6h | 36h | 6mo. |
| 10°C | 6h | 24h | 5h | 24h | 6mo. |
| 20°C | 3h | 8h | 4h | 8h | 6mo. |
| 30°C | 2h | 6h | 2h | 6h | 6mo. |
*The maximum recoat interval depends on the exposure environment and the end use of the coating.
All surfaces to be coated must be clean, dry and free of contaminants. Before application, all surfaces must be assessed and prepared in accordance with ISO 8504:2000. When used as a primer, blast clean the substrate to Sa 2½, with surface roughness 40–75 µm. Before rust removal, remove all oil and weld spatter and grind welds and sharp edges. Areas of the coating damaged mechanically and showing localised rust must be spot blast cleaned to Sa 2½ or cleaned with power tools to St 3 before local repair. When applied over other existing coatings, remove chalk, zinc salts, grease and other contaminants by suitable methods. When applied over inorganic zinc silicate primers or metal spray surfaces, use an approved tie coat or transitional coat.
1. During application, ensure ventilation and exhaust, keep away from ignition sources, and wear protective equipment such as masks and gloves; maintain adequate ventilation during curing. 2. When mixing, first stir the base thoroughly, then add the hardener in the specified ratio and mix evenly; adjust the thinner quantity according to application needs and temperature, mix thoroughly and allow induction. 3. When overcoating inorganic zinc silicate coatings, seal with a transition coat first; apply this product only after the transition coat is hard-dry, otherwise the sealing effectiveness is reduced. 4. Excessive thinning reduces sag resistance and slows curing. 5. Excessive film thickness adversely affects drying/curing, recoating and handling time. For better coating performance, when the film thickness exceeds 200 µm, apply in multiple coats to improve film density. Avoid a single over-thick coat on edges, corners and welds; if over-thick, extend the recoat interval for subsequent coats to allow solvent release, otherwise the coating may crack in service. 6. If the coating chalks after long-term exposure, wash with high-pressure water or abrade the surface before applying subsequent coats. 7. Roller application cannot achieve high film thickness and a continuous film in one pass; multiple coats are required. 8. During application and curing, the substrate temperature must be at least 3 °C above the dew point, and relative humidity must not exceed 85%. 9. In steel structure shops requiring fast recoating, the fast-drying hardener can be used below 20 °C. In other anticorrosive maintenance work, the fast-drying hardener can be used below 15 °C. Above 20 °C, the fast-drying hardener is not recommended as the pot life is shortened. If it must still be used as the temperature rises, allow for the shortened pot life or switch to the general-purpose hardener. 10. Cutting structures coated with this product produces fumes and dust; take appropriate protection. 11. During work breaks, do not leave paint in the hose, spray gun or spray equipment. Flush all equipment thoroughly with thinner. If the break is too long, mix a fresh batch of paint for application. 12. Clean all equipment with thinner immediately after use. Flushing spray equipment regularly during work is good practice. Cleaning frequency depends on spray volume, temperature and spraying time including interruptions. 13. Dispose of leftover paint and empty cans in accordance with local regulations.
| 20 L per unit | Base 15.4 L | Curing agent 4.6 L |
Store sealed in a ventilated, cool, dry place away from ignition sources; ideal storage temperature 5–35 °C. Minimum 12 months
1. For the coating and its recommended thinners, see the safety sheets and the safety data of the relevant materials. This is a solvent-borne coating; avoid inhaling spray mist and solvent vapours, and avoid exposing skin and eyes and contact with uncured paint as far as possible. 2. All work related to the application and use of this product must comply with the relevant national health, safety and environmental standards and regulations. 3. If welding or flame cutting is required on metal coated with this product, dust and fumes will be generated; use appropriate personal protective equipment and adequate local ventilation. 4. If in doubt about the suitability of this product, consult the company.
The information provided in this product data sheet is based on laboratory test results that we consider accurate, and is provided for application guidance only. All recommendations and advice given by T&H on the use of T&H products, whether in technical documents, special consultation or otherwise, are based on information we consider most reliable. Our products and the information provided are intended for users with the necessary knowledge and industrial experience, and it is for these end users to determine whether the products are suitable for their use. T&H cannot control the quality and condition of the substrate, nor the various factors affecting the use of the product. Therefore, T&H accepts no liability for any loss, injury or damage arising from the use of our products or from reliance on this product data sheet (unless otherwise agreed in writing). Data in this product data sheet may be revised as necessary based on practical experience and continued product development.
Information is subject to the manufacturer's latest version; the manufacturer's latest TDS prevails.
The technical parameters on this page are taken from the product's original manufacturer technical datasheet, the copyright of which belongs to the manufacturer. If a rights holder considers the presentation inappropriate, contact us for verification and handling.
Packaging specifications and batch lead times are subject to actual availability. PleaseContact Uscontact us for project-based calculation.